Step into a modern weaving shed and the first thing you notice is the sound. It is a steady, sharp hiss, repeated hundreds of times a minute. That hiss is compressed air carrying a thread across the loom. There is no shuttle and no rapier. A short blast of air does the work, and it does it at a speed that older looms could not match. This machine is the air jet loom, and it makes a large share of the world’s woven shirting, bedsheet and dress fabric.
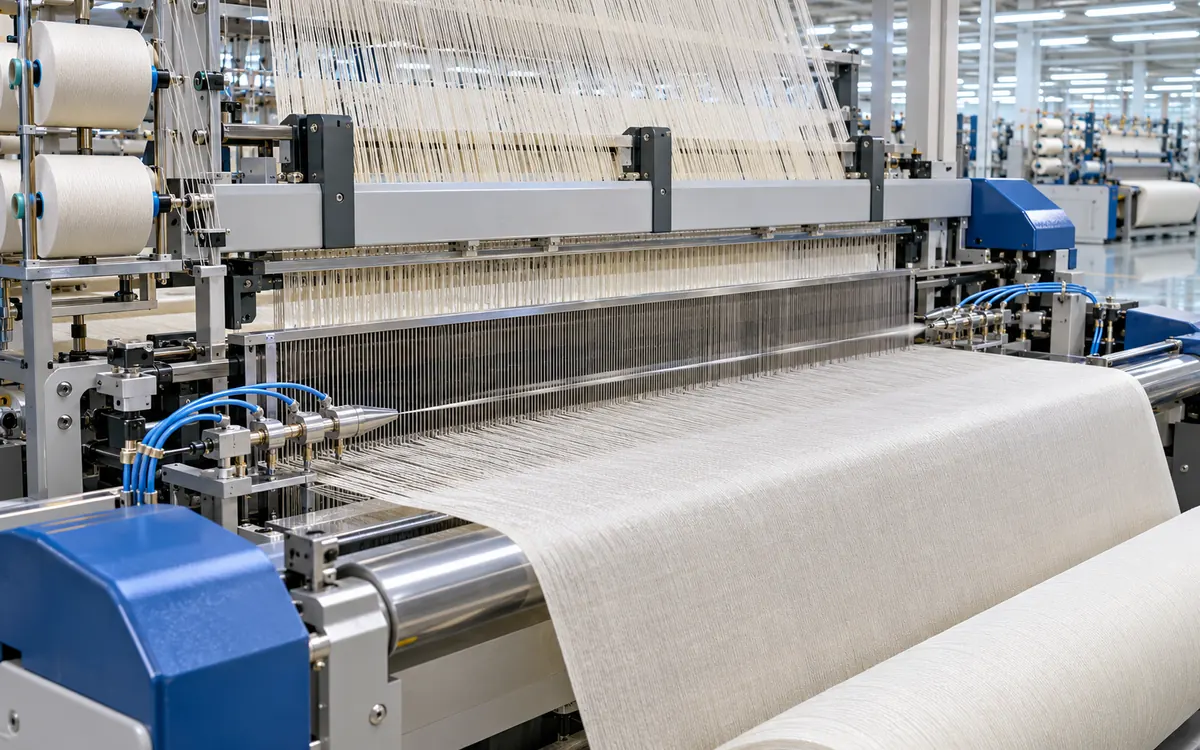
This guide explains the working principle of the air jet loom, its parts and the steps in one weaving cycle. It covers speed, air use and cost, which fabrics suit it, how it differs from rapier and water jet looms, and the faults you will meet. It includes worked examples for loom output, weft insertion rate and compressed air cost. For the basics of how any loom works, read our guide on the weaving process and our article on the parts of a loom.
What is an air jet loom
An air jet loom is a shuttleless weaving machine that inserts the weft yarn by blowing it through the warp shed with compressed air. The weft travels across the full width of the fabric in a few milliseconds. After each pick, a cutter cuts the weft, the reed pushes it into the fabric and the cycle begins again.
Because the weft carrier is air and not a heavy shuttle or rapier, the moving mass is low. That allows high speeds, low vibration and less wear on parts. The price is a steady need for compressed air, which uses a lot of electricity.
Working principle in simple words
Think of a long, thin straw. If you blow a puff of air along it, a light thread inside will be carried to the other end. The loom does the same thing, but the straw is made of the open warp shed and a special reed, and the puff is carefully timed and shaped.
- A measured length of weft is pulled from a package and stored on a feeder.
- A main nozzle grips the weft end and blasts air to launch it into the shed.
- The weft would slow down quickly in open air, so a row of relay nozzles along the reed fire in order, one after another, to keep it moving. The relay blasts form a moving air stream that follows the yarn.
- A sensor at the far side confirms the weft has arrived.
- The reed beats the weft against the cloth edge.
- A cutter cuts the weft at the near side, ready for the next pick.
All of this happens in one turn of the main shaft, which may take less than 0.1 second.
Main parts of an air jet loom
| Part | What it does |
|---|---|
| Weft package and feeder (prewinder) | Holds the yarn and measures out the exact length for each pick |
| Weft brake and accumulator | Controls the tension and stops the yarn at the right moment |
| Main nozzle | Gives the first push of air that launches the weft |
| Relay (auxiliary) nozzles | Fire along the shed to keep the yarn moving |
| Profiled (tunnel) reed | A reed with a groove that forms a guiding channel for the air and yarn |
| Weft sensors (detectors) | Check that the weft arrives at the right time |
| Stretch nozzle | Holds the weft straight just after it arrives |
| Cutters | Cut the weft at the feed side |
| Selvedge motion | Forms the edge of the fabric, by leno or tuck-in methods |
| Shedding motion | Cam, dobby or jacquard. Opens the warp shed |
| Warp beam and let-off | Releases warp yarn with steady tension, usually electronically controlled |
| Take-up and cloth roller | Draws the fabric forward and winds it |
| Warp stop motion | Stops the loom if a warp end breaks |
| Valves and air tank | Control and supply compressed air to the nozzles |
| Electronic control unit | Sets timing, speed and pressure, and records data |
The profiled reed is a key feature. The channel in the reed keeps the air stream narrow and straight, so the weft does not fly out into the warp threads. Reed dents must be clean and smooth, or the weft will catch.
One weaving cycle: step by step
| Step | What happens |
|---|---|
| 1. Shed opens | Warp ends separate into an upper and a lower sheet |
| 2. Feeder releases | The measuring unit lets out the right length of weft |
| 3. Main nozzle fires | A blast of air carries the weft into the reed channel |
| 4. Relay nozzles fire in order | Each group of nozzles blows briefly as the weft tip passes |
| 5. Weft arrives | The sensor at the arrival side confirms the pick |
| 6. Stretching | The stretch nozzle pulls the weft straight |
| 7. Beat-up | The reed moves forward and places the pick into the fabric |
| 8. Cutting | The cutter cuts the weft at the feed side |
| 9. Shed changes | The warp ends change position for the next pick |
| 10. Fabric advances | The take-up moves the fabric forward by one pick spacing |
If the sensor does not detect the weft in time, the loom stops. The operator then clears the broken weft from the shed and restarts. Modern looms often try to fix the pick automatically.
Speed and capacity
Air jet looms are among the fastest looms. Typical working speeds are around 600 to 1,000 picks per minute on commonly used widths, and some high-speed machines run faster on narrow, light fabrics. The speed depends on the yarn, the width and the fabric. Wider looms run slower because the weft must travel farther.
A useful measure is the weft insertion rate, which is how many metres of weft the loom inserts per minute.
Weft insertion rate (m/min) = picks per minute × reed width (m)
Worked example 1: weft insertion rate
A loom with a reed width of 2.3 metres runs at 700 picks per minute.
- Insertion rate = 700 × 2.3 = 1,610 m per minute
A narrower loom of 1.9 m width at 800 picks per minute gives 800 × 1.9 = 1,520 m per minute. The wider loom actually inserts more weft per minute, even at a lower speed. Mills quote this number to compare machines of different width.
Worked example 2: fabric output
Production (m/hr) = (picks per minute × 60 × 0.0254) ÷ PPI × efficiency
Here 0.0254 converts inches to metres. A mill weaves a shirting fabric on a 700 picks per minute loom. The fabric has 60 picks per inch (PPI), and loom efficiency is 90 percent.
- Picks per hour = 700 × 60 = 42,000
- Metres at 100 percent = 42,000 × 0.0254 ÷ 60 = 17.78 m per hour
- At 90 percent = 17.78 × 0.90 = 16.0 m per hour
- Per 24-hour day = 16.0 × 24 = 384 metres per loom
For a shed of 120 looms, the daily output is 384 × 120 = 46,080 metres. If efficiency drops by 3 points, to 87 percent, the output per loom falls to 17.78 × 0.87 × 24 = 371 metres, a loss of 13 metres per loom per day, or 1,560 metres across the shed. That is why mills watch stops closely. For a wider look at cost, see our guide on the calculation of weaving cost and profit.
Worked example 3: cost of compressed air
Air is the main running cost of an air jet loom. Suppose one loom uses 1.4 normal cubic metres per minute of compressed air at about 6 to 7 bar while running. Compressors use roughly 6 to 7 kilowatts of electric power for every cubic metre per minute of air they deliver at this pressure. Take 6.5 kW per m³/min as a working figure. Your own plant should measure the real numbers.
- Power for the loom’s air = 1.4 × 6.5 = 9.1 kW
- Energy per day = 9.1 × 24 = 218 kWh per loom
- Energy per metre of cloth = 9.1 kW ÷ 16.0 m per hour = 0.57 kWh per metre
At an electricity price of 10 currency units per kWh, air costs 0.57 × 10 = 5.7 units per metre. For 100 looms, the compressors use about 910 kW. A leak of 10 percent in the air system would waste 91 kW, which at 10 units is 910 units per hour, or about 21,840 units a day. Leak checks, correct pressure settings and good compressor control give some of the fastest savings in a weaving mill. For more energy-saving ideas see our article on the factory energy efficiency checklist.
What fabrics suit an air jet loom
| Good fit | Why |
|---|---|
| Cotton and polyester-cotton shirting and sheeting | Medium counts and balanced yarns insert reliably |
| Poplin, voile, lawn, cambric | Light, fine yarns are easy to carry by air |
| Plain, twill and sateen weaves | Simple shedding works at high speed |
| Filament polyester and nylon | Smooth yarns fly well |
| Denim in some mills | With the right yarn and settings. See twill weave |
| Technical fabrics | Glass and special yarns on dedicated machines |
| Less suitable | Why |
|---|---|
| Very coarse or heavy yarns | Air cannot carry them well |
| Fancy yarns with slubs or loops | They catch in the reed |
| Many colours in the weft | Standard machines carry only four to eight colours, rapier looms are more flexible |
| Very hairy yarns | Fibre drag slows the weft |
Air jet loom vs rapier loom vs water jet loom
| Point | Air jet | Rapier | Water jet |
|---|---|---|---|
| Weft carrier | Compressed air | Rigid or flexible rapier | A jet of water |
| Speed | Very high | Medium to high | Very high |
| Weft colours | Limited | Many | Limited |
| Yarn range | Medium counts, smooth | Very wide | Smooth, water-repellent filament |
| Running cost | Compressed air is high | Lower | Water and drying/treatment cost |
| Fabric type | Light to medium | Light to heavy, fancy | Light filament fabrics |
| Noise | High | Lower | Medium |
| Best for | Mass production of basic cloth | Flexible, fancy and home textiles | Polyester and nylon filament cloth |
Read more in our guide to the rapier loom. For older hand-operated methods see the handloom guide.
What is a water jet loom
A water jet loom works the same way as an air jet loom, but uses a thin jet of water to carry the weft. It is limited to yarns that do not absorb water, such as polyester and nylon filament, because wet cotton would swell and cause problems. The water leaves a damp fabric that must be dried, and the used water needs treatment. It runs at very high speeds on light fabrics and uses less power than air, but needs a water system. See our article on the water treatment plant process in industry for the treatment side.
Advantages of air jet looms
- Very high speed and output per loom
- Low vibration and less mechanical wear
- Fewer moving parts than shuttle looms
- Consistent quality and good fabric appearance
- Wide fabric widths possible
- Low labour per metre, with each weaver handling many looms
- Good electronic control and data recording
Limitations of air jet looms
- High compressed air use and energy cost
- Limited colour change in the weft
- Not suited for very heavy, fancy or weak yarn
- Noise level needs ear protection
- Needs clean, dry, oil-free air
- Higher machine price than basic looms
- Sensitive to yarn quality and humidity
Factors that affect performance
- Yarn quality. Even, strong yarn with few thick and thin places and low hairiness flies better and breaks less.
- Air pressure and timing. Too little pressure leaves the weft short. Too much wastes energy and can whip the yarn.
- Reed and nozzle condition. Bent dents or blocked nozzles cause weft stops.
- Humidity. About 60 to 70 percent relative humidity is common in weaving sheds for cotton, since dry air raises static and breaks. Follow your yarn supplier’s advice.
- Warp preparation. Good sizing and clean beams reduce warp stops. See the section on sizing in our guide on the weaving process.
- Loom settings. Shed timing, weft arrival angle and beat-up settings must match the fabric.
- Air quality. Moisture, oil or dirt in the air can stain fabric and block nozzles.
Common faults and fixes
| Fault | Likely cause | Fix |
|---|---|---|
| Weft stops at the arrival side | Low air pressure, worn nozzles, hairy yarn | Raise pressure, clean or replace nozzles, check yarn |
| Short pick (weft does not arrive) | Blocked relay nozzle or reed channel | Clean the channel and nozzles |
| Broken pick or double pick | Wrong feeder length or cutter timing | Adjust feeder and cutter |
| Warp breaks | Weak or poorly sized yarn, rough reed | Improve sizing and clean the path |
| Reed marks | Bent dents, wrong tension | Replace the reed, adjust tension |
| Loose weft ends in selvedge | Poor tuck-in or cutter timing | Reset selvedge motion |
| Oil stains | Dirty air or lubrication leaks | Fit better air filters, check oilers |
| Thin places or bars | Variation in weft tension | Adjust brake and feeder, check yarn |
| High energy bills | Leaks, high pressure | Audit the air system |
For other kinds of cloth faults and how to grade them, see our guide on fabric defects.
Maintenance tips
- Clean lint from the reed, nozzles and sensors every shift.
- Drain and check the air dryers and filters.
- Check the air system for leaks with an ultrasonic detector or soapy water.
- Replace worn cutters and nozzles on schedule.
- Keep a log of stops by cause. Patterns show where to act.
- Train weavers and mechanics on the control panel settings.
Final thoughts
The air jet loom shows how a simple idea, a puff of air, can be used with great precision. It gives mills speed, output and steady quality for everyday fabrics. In return it asks for good yarn, clean air and close attention to energy use. If you run one, measure your air use, fix leaks, log your stops and keep your reeds and nozzles clean. If you are choosing a loom, match the machine to the fabrics you make, not only to the top speed on the brochure.
Frequently asked questions
It is a shuttleless loom that inserts the weft yarn into the warp shed with a jet of compressed air.
A main nozzle launches the measured weft yarn, relay nozzles along the reed keep it moving, a sensor checks that it arrives, then the reed beats it into the fabric and a cutter cuts the yarn.
Typical speeds are about 600 to 1,000 picks per minute, and some machines run faster on light, narrow fabrics.
Mostly cotton, polyester and blends in plain, twill and sateen weaves, including shirting, sheeting and light denim.
An air jet loom uses compressed air to carry the weft and works with most yarns. A water jet loom uses a jet of water and is limited to non-absorbent filament yarns like polyester.
Compressed air is costly to make, and the nozzles use it hundreds of times each minute. Compressors use the most of the electricity.
Not as well as a rapier or projectile loom. Heavy, coarse yarns are hard to carry with air.