
Every garment factory runs on a number it rarely talks about: the time a job should take. That number sets the price of a piece, the target of a line, the pay of an operator and the capacity you promise a buyer. If it is wrong, everything built on it is wrong. The tools used to find that number are called work measurement techniques.
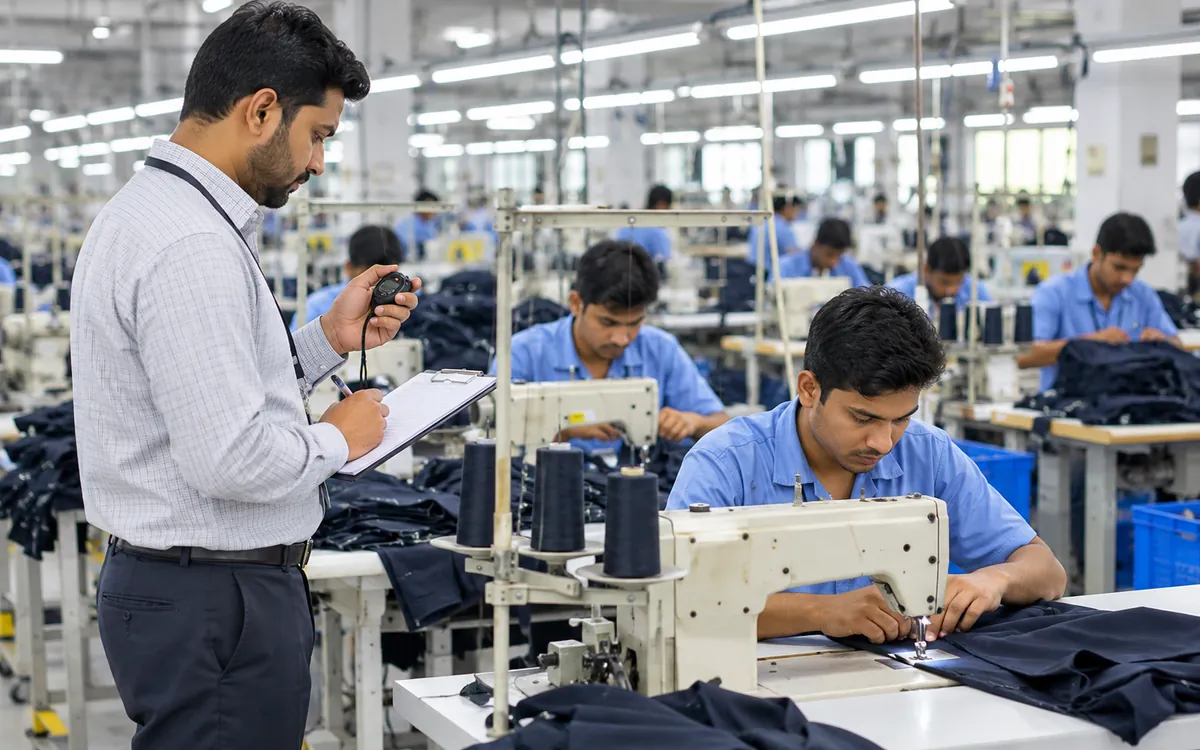
This guide explains the main work measurement techniques used in apparel: time study, work sampling, predetermined motion time systems and standard data. It includes a full worked example of a stopwatch study, with the arithmetic shown step by step. If you are new to the idea of a standard time, start with our guides on SAM vs SMV and how to calculate SAM.
What work measurement is
Work measurement is the process of finding how long a qualified worker, working at a normal pace, takes to do a defined task. The result is called the standard time. In garments, it is also called the standard minute value (SMV) or standard allowed minute (SAM).
Work measurement answers questions such as:
- How many pieces should one operator make in an hour?
- How many operators does this style need?
- What is a fair price for this operation?
- Is the line balanced?
- How efficient is the line against the standard?
Without a measured time, the answers are guesses. For a closer look at the standard minute and why it matters, read our guide on the standard minute value in garments.
The main techniques
There are four groups of work measurement techniques.
| Technique | How it works | Best for |
|---|---|---|
| Time study | A stopwatch study of the actual job | Repeated jobs with short cycles |
| Work sampling | Random observations of what workers are doing | Long or irregular jobs, utilization |
| Predetermined motion time systems (PMTS) | Times from tables of basic motions | New styles, before production |
| Standard data | Times collected from past studies | Fast estimates for similar jobs |
Each has a place. Large factories usually use more than one.
Time study
What it is
Time study is the best known technique. An industrial engineer watches an operator do the job and records the time of each cycle with a stopwatch or a digital timer. The observed time is then adjusted for the operator’s pace and for allowances, to give the standard time.
Steps in a time study
- Select the job. Choose an operation and define its start and end.
- Break it into elements. Split the operation into small steps, such as pick up, align, sew and trim.
- Choose the operator. Pick an average, trained operator, and tell them what is happening.
- Record the times. Time each element over several cycles.
- Rate the operator. Judge how fast the operator worked compared with a normal pace.
- Calculate normal time. Multiply the observed time by the rating.
- Add allowances. Add time for rest, personal needs and delays.
- Find the standard time.
A worked example
Let us time the operation “close side seam” on a woven shirt. We watch one operator for 10 cycles and record the cycle time in seconds.
| Cycle | Time (s) |
|---|---|
| 1 | 38 |
| 2 | 40 |
| 3 | 37 |
| 4 | 41 |
| 5 | 39 |
| 6 | 40 |
| 7 | 38 |
| 8 | 42 |
| 9 | 39 |
| 10 | 40 |
| Total | 394 |
Step 1: Average observed time. 394 divided by 10 cycles gives 39.4 seconds.
Step 2: Rating. The engineer judges that the operator worked at 90 percent of the normal pace, which means slightly slow. Rating uses a scale where 100 is normal.
Step 3: Normal time. Multiply the average by the rating: 39.4 × 0.90 = 35.46 seconds.
Step 4: Allowances. The factory uses these allowances:
- Personal needs: 5 percent
- Fatigue: 5 percent
- Delay and machine allowance: 4 percent
- Total: 14 percent
Step 5: Standard time. Multiply normal time by 1.14: 35.46 × 1.14 = 40.42 seconds. Divide by 60 to convert to minutes: 40.42 / 60 = 0.674 minutes.
So the SMV for this operation is about 0.67 minutes. A fully efficient operator could make 60 / 0.674 = about 89 pieces per hour on this operation.
How many cycles do you need
Ten cycles is not always enough. If the times vary a lot, you need more. A common formula for 95 percent confidence and a 5 percent error is:
n = [ 40 × √(n′ × Σx² − (Σx)²) / Σx ]²
where n′ is the number of readings taken, x is each reading and Σ means “sum of”. For our data, Σx = 394 and Σx² = 15,544, and n′ = 10. Putting these numbers in gives n of about 2.1, so three cycles would already be enough. Our 10 readings are more than needed. If your times were very scattered, the formula would call for more.
Rating
Rating is the hardest part. It is a judgement. The engineer compares the pace they see with the pace of a trained, motivated operator working steadily. Rating scales differ. Many factories use a scale where 100 is normal and 60 is very slow. Training and practice improve rating consistency. Many companies run rating exercises with videos so that engineers agree with each other.
Allowances
Allowances give the operator time for things the study does not capture.
- Personal allowance: Visits to the restroom or a drink of water.
- Fatigue allowance: Rest for long or heavy tasks.
- Delay allowance: Waiting for work, thread changes and small machine stops.
- Special allowance: Extra time for a hot or awkward task.
The right allowance percentage depends on the factory’s policy and the job. Do not copy a number from another factory without checking.
Work sampling
What it is
Work sampling, also called activity sampling, takes random snapshots of workers or machines and records what each one is doing. After enough snapshots, the percentages show how time is spent.
It is useful for:
- Finding how much of the day an operator is working versus waiting.
- Measuring machine utilization.
- Setting allowances.
- Studying jobs with long cycles, such as cutting or finishing, where a stopwatch is hard to use.
Example
An engineer visits a sewing line at random times, 20 times a day for 15 days. At each visit, they note how many of 10 operators are working, waiting or absent. Suppose in 300 observations, operators were working 225 times. Working share = 225 / 300 = 75 percent.
How many observations are enough? A common formula is:
n = 4 × p × (1 − p) / L²
where p is the share found, and L is the accuracy you want. For p = 0.75 and L = 0.05 (5 percent), n = 4 × 0.75 × 0.25 / 0.0025 = 300. So 300 observations give about 95 percent confidence that the true share lies within plus or minus 5 percent.
Pros and cons
Work sampling is cheap and does not disturb workers. But it does not give detailed time for each element, and it needs many observations to be accurate.
Predetermined motion time systems (PMTS)
What it is
A PMTS gives a time to each basic motion, such as reach, grasp, move, position and release. The times were measured in many studies and put in tables. To find a job’s time, the analyst breaks the job into motions and adds up the table times.
PMTS does not need a stopwatch or a rating. This is a big advantage in garments, because you can set the time before the style reaches the floor, during sample making.
Time units
The most known system is MTM, or methods-time measurement. Its unit is the TMU, the time measurement unit. One TMU equals 0.00001 hour, which is 0.036 seconds. So 100 TMU equal 3.6 seconds.
Common systems
- MTM-1: The detailed original system. Slow to apply but very accurate.
- MTM-2 and MTM-3: Simpler versions that group motions.
- MOST (Maynard Operation Sequence Technique): Uses sequence models and index values. Fast to apply.
- GSD (General Sewing Data): A system built for the sewing industry, based on motion times.
Many garment buyers and big groups use PMTS to set SMVs for new styles. Their software contains a library of motions and operations.
Converting TMU to time
The tables themselves are licensed, so we will not copy them here. What you can do is convert any total. Suppose an analyst adds up the table values for a short sewing task and gets 150 TMU. The time is 150 × 0.036 = 5.4 seconds. A task of 1,000 TMU is 36 seconds, or 0.6 minutes. Once the total is in seconds, you add allowances in the same way as in a time study.
Pros and cons
PMTS is consistent and does not depend on an operator’s pace. But the training is long and the software or licenses cost money. It also needs careful method description. A small mistake in the method gives a wrong time.
Standard data
What it is
Standard data is a library of times for common elements, built from past time studies or PMTS. For example, “sew 10 cm of straight seam”, “pick up a bundle” and “turn a collar”. When a new style arrives, the engineer builds the time by adding up library values.
Example
Suppose the library says:
- Sewing time per cm of straight seam: 0.06 seconds, including machine run time.
- Handle time to pick up, align and turn per seam: 8 seconds.
For a seam of 60 cm, the time would be 8 + (60 × 0.06) = 8 + 3.6 = 11.6 seconds. Add allowances and the SMV follows.
Pros and cons
Standard data is quick and consistent. It is the fastest way to estimate costs. But the library has to be built and kept up to date. If the factory changes machines or methods, the standard data has to change too.
Synthetic and analytical estimating
Some factories also use estimating. An experienced engineer estimates times based on knowledge of similar jobs. It is quick but depends on the person. It is best used for rough costing only, not for line targets.
Choosing a technique
| Situation | Suggested technique |
|---|---|
| New style, pre-production | PMTS or standard data |
| Existing operation, repeated work | Time study |
| Utilization and delay study | Work sampling |
| Fast quotation | Standard data or estimating |
| Dispute on a rate | Time study with rating review |
Most factories combine them. For example, a buying house might use PMTS on a new style, then confirm with a time study in the first week of production.
From standard time to line planning
The measured time feeds many planning decisions. If a style has a total SMV of 12 minutes and the line makes 800 pieces a day at 8 hours per shift, with 60 operators at 85 percent efficiency, one can check the plan.
Total minutes needed = 800 × 12 = 9,600 minutes. Available minutes = 60 operators × 480 minutes × 0.85 = 24,480 minutes.
The line has more capacity than needed, so the plan is feasible, or the line could be cut to about 24 operators for this target. These numbers are an example only. Your plan will use your own numbers. For machine planning, see our guide on machine requirement calculation for a garment line.
Common mistakes
- Timing the wrong operator. Choose someone close to average.
- Poor element breaks. Elements should have clear start and end points.
- Too few cycles. Check variation and use the sample formula.
- Biased rating. Train engineers and cross check.
- Ignoring method. Fix the method first, then time it.
- Copying allowances. Set them for your factory.
- Forgetting machine time. For long machine cycles, separate machine time from handling time.
- Not updating standards. Re-study when the method changes.
Where IE fits
Work measurement is a core duty of the industrial engineering department. IEs set times, balance lines, study methods and track efficiency. If you want to see the wider role, read our guide on the roles of industrial engineering in a garments factory and the list of necessary IE terms in the apparel industry.
Final thoughts
Work measurement turns opinion into numbers. A stopwatch study gives a real time for a real job. Work sampling shows where the day goes. PMTS and standard data let you set times before the first piece is sewn. Choose the one that fits the job, check your sample size, rate carefully and set allowances for your own factory. A good standard time is the base of fair pay, honest prices and a line plan you can trust.
Frequently asked questions
The main techniques are time study, work sampling, predetermined motion time systems such as MTM and MOST, and standard data.
Normal time is the observed time adjusted for the operator’s pace. Standard time is normal time plus allowances for rest, personal needs and delays.
A TMU is a time measurement unit used in MTM. One TMU is 0.00001 hour, or 0.036 seconds.
It depends on how much the times vary. Use the sample size formula for the confidence level you need. Ten cycles is a common starting point for short operations.
Rating compares the operator’s pace to a normal pace. A rating of 90 means the operator worked at 90 percent of normal.
They suit different jobs. Work sampling is better for long or irregular tasks and for studying utilization. Time study is better for short, repeated operations.
A predetermined motion time system or standard data works well, because you can set the time before production starts.
