Every garment target, every costing sheet and every efficiency report in a factory rests on one small number. It is the time a trained operator needs to make a piece at a normal pace. That number is the Standard Allowed Minutes, or SAM. If it is right, targets are fair and prices are safe. If it is wrong by even five percent, the error runs through everything built on top of it.
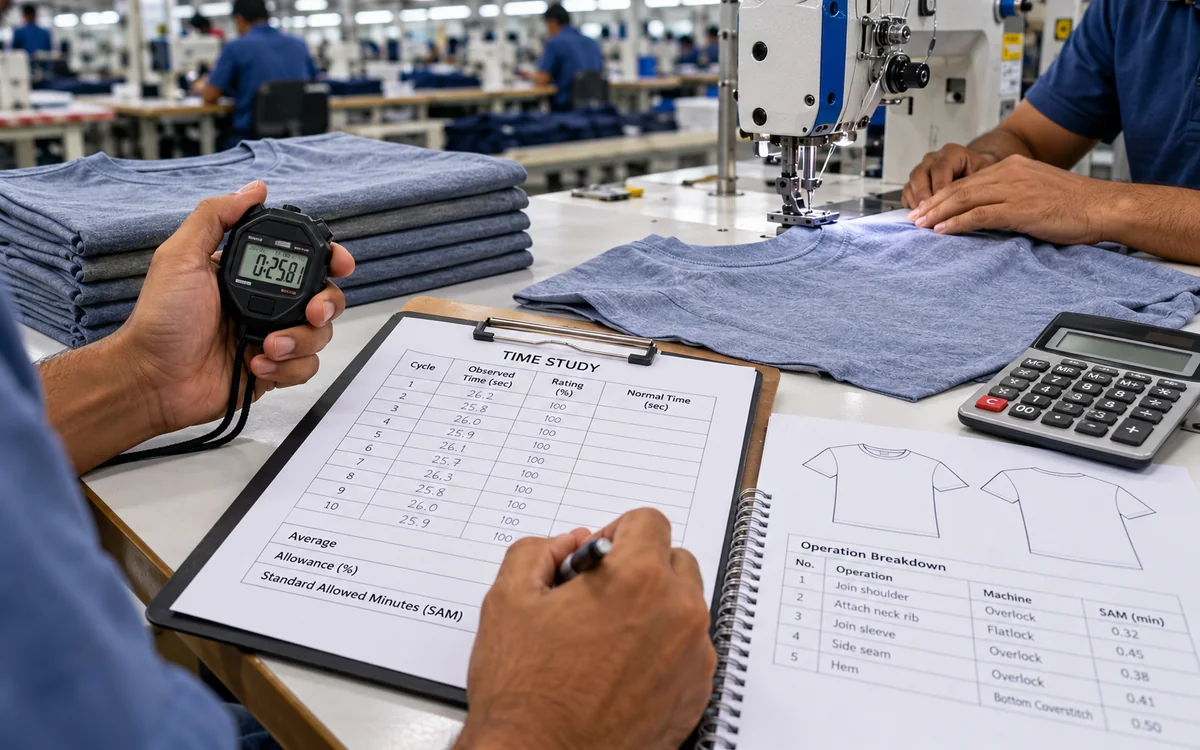
This guide shows how to calculate standard allowed minutes from scratch. You will see the formula, the steps of a time study, how rating and allowances work and a full worked example, first for one operation and then for a whole T-shirt. We also show how SAM turns into a line target, an efficiency figure and a cost. For the definition and background, see our existing pages on standard allowed minutes and on SAM versus SMV. This article focuses on the calculation itself.
What SAM means in one paragraph
SAM is the standard time, in minutes, to complete a task or a whole garment, including allowances for rest and unavoidable delay. It assumes a trained operator, working at a normal pace, with the right machine, method and material. Many factories use the terms SAM and SMV (standard minute value) for the same thing. A few use SMV for the basic time without allowances. Always check how your buyer or your factory defines it. Our page on the standard minute value explains the second view.
The formula
Basic time = average observed time × rating ÷ 100
Standard time (SAM) = basic time × (1 + allowance %)
Three ideas sit inside these lines.
- Observed time is what you measure with a stopwatch or a video.
- Rating corrects for the pace of the operator you watched. If the person works at a normal pace, the rating is 100 percent. If faster, it is above 100. If slower, below.
- Allowance adds time for personal needs, fatigue and small delays that cannot be avoided.
The result in seconds is divided by 60 to give minutes.
Step 1: Break the garment into operations
List every operation in the order of work. An operation is a task done by one operator on one machine, such as “join shoulders” or “attach neck rib”. Write a clear description, the machine type, the stitch type and any special tool. This list is the operation breakdown. See our example of an operation breakdown and SMV for a knit T-shirt.
Break each operation into small elements if it is long. Elements make it easier to spot slow steps and to compare methods. A typical element list for “attach sleeve” would be pick up parts, align, sew, trim and place aside.
Step 2: Fix the method before you time it
Time study measures a method. If the method changes, the time changes. Before timing, make sure the operator uses the standard method with the right machine, attachment, needle, thread and stitch density. Also check that the workplace is set up correctly and the material is of normal quality. Timing a poor method produces a poor standard.
Step 3: Choose the operator and the sample
Pick a trained operator who is neither the fastest nor the slowest. Explain that the study is to set a standard for the job and not to judge the person. Observe at least 10 cycles for short operations. For very short cycles, more cycles give a steadier average. For long cycles, fewer may be enough, but never base a standard on one or two readings.
Step 4: Time the cycles
Use a stopwatch, a timing app or a video with a time stamp. Record the time for each full cycle of the operation. If an unusual event happens, such as a thread break, note it and exclude that cycle from the average, as it will be covered by allowances. Note the time for each element too, if you are using element timing.
Step 5: Judge the rating
Rating is the study person’s judgement of the operator’s pace compared with a normal pace. The scale used in industry sets 100 as normal. Some systems use 60-80-100-120 anchors. A rating of 90 means the operator is working at 90 percent of a normal pace. Rating is a skill. It needs training and practice, ideally with reference videos so that different engineers reach similar ratings. Consistency matters more than any single number.
Step 6: Decide the allowances
Allowances are extra time to cover things that are part of real work but not part of the basic task. Common groups are:
| Allowance | What it covers | Typical range |
|---|---|---|
| Personal | Drinking water, toilet, short breaks | About 4 to 6 percent |
| Fatigue | Tiring work, long standing, awkward posture, heat | About 4 to 10 percent, depending on conditions |
| Delay or contingency | Small unavoidable stops such as thread breaks, needle changes, waiting for bundle | About 2 to 5 percent |
| Bundle or handling | Picking and moving bundles | Often included in the others, or set separately |
| Machine allowance | Machine-controlled time where the operator waits | Added per operation if relevant |
| Special | Training, cleaning, setting up | Set by the factory |
Total allowances in garment factories are often in the range of 10 to 20 percent. The exact figures differ by factory, buyer standard and country. Use the figure agreed with your management and buyer, and write it in the study.
One caution. Some companies add the allowance on top of basic time (multiply by 1.15 for 15 percent). Others define the allowance as a share of the final standard time (divide by 0.85 for 15 percent). The second gives a slightly higher SAM. Pick one rule and apply it everywhere.
Worked example 1: SAM for one operation
The operation is “attach sleeve” on a knit T-shirt, using a 4-thread overlock machine.
Observed times (seconds) for 10 cycles
52, 55, 50, 58, 54, 53, 51, 56, 55, 54
Average observed time
- Sum = 52 + 55 + 50 + 58 + 54 + 53 + 51 + 56 + 55 + 54 = 538
- Average = 538 ÷ 10 = 53.8 seconds
Rating
The operator worked at a pace judged to be 90 percent of normal.
Basic time
- 53.8 × 90 ÷ 100 = 48.42 seconds
Allowances
- Personal 5 percent, fatigue 6 percent, delay 4 percent, total 15 percent
Standard time (add-on method)
- 48.42 × 1.15 = 55.68 seconds
- In minutes: 55.68 ÷ 60 = 0.928 minutes
Standard time (share-of-standard method)
- 48.42 ÷ (1 − 0.15) = 56.96 seconds
- In minutes: 56.96 ÷ 60 = 0.949 minutes
The two methods differ by about 2 percent. This is why the factory must state its rule.
So the SAM for this operation is about 0.93 minutes with the add-on method.
Worked example 2: SAM for a whole T-shirt
Once every operation has its standard time, the garment SAM is the sum. Here is a sample list for a basic round-neck T-shirt. The figures are illustrative.
| No. | Operation | Machine | SAM (min) |
|---|---|---|---|
| 1 | Join shoulders | 4-thread overlock | 0.42 |
| 2 | Make neck rib loop | Lockstitch | 0.30 |
| 3 | Attach neck rib | 4-thread overlock | 0.95 |
| 4 | Attach back neck tape | Lockstitch | 0.55 |
| 5 | Topstitch neck | Coverstitch | 0.70 |
| 6 | Attach sleeves | 4-thread overlock | 0.93 |
| 7 | Side seam with care label | 4-thread overlock | 1.10 |
| 8 | Hem sleeves | Coverstitch | 0.60 |
| 9 | Hem bottom | Coverstitch | 0.70 |
| 10 | Attach main label | Lockstitch | 0.35 |
| 11 | Thread trimming | Hand | 0.45 |
| Sewing SAM | 7.05 | ||
| 12 | Finishing, iron, check, fold, pack | Hand | 1.10 |
| Total garment SAM | 8.15 |
Check the sum of the sewing operations: 0.42 + 0.30 + 0.95 + 0.55 + 0.70 + 0.93 + 1.10 + 0.60 + 0.70 + 0.35 + 0.45 = 7.05. Adding finishing, 7.05 + 1.10 = 8.15. Cutting is usually counted separately.
From SAM to a line target
The target for a day follows from SAM.
Target = operators × working minutes × efficiency ÷ SAM
Take a line of 25 operators, 480 working minutes and a planned efficiency of 70 percent, using the sewing SAM of 7.05.
- Available minutes = 25 × 480 = 12,000
- Productive minutes = 12,000 × 0.70 = 8,400
- Target = 8,400 ÷ 7.05 = 1,191 pieces
From SAM to efficiency
Efficiency compares the minutes earned with the minutes available.
Efficiency % = output × SAM ÷ (operators × working minutes) × 100
If the line makes 1,000 pieces:
- Earned minutes = 1,000 × 7.05 = 7,050
- Efficiency = 7,050 ÷ 12,000 × 100 = 58.75 percent
From SAM to operators needed
If the plan calls for 1,200 pieces a day at 70 percent efficiency:
- Operators = 1,200 × 7.05 ÷ (480 × 0.70) = 8,460 ÷ 336 = 25.2
So the plan needs 26 operators, rounded up, and the line balance decides how they are spread across operations.
From SAM to cost
If the factory cost per available minute, including wages and overheads, is 0.03 dollars:
- Conversion cost per piece = SAM ÷ efficiency × cost per minute
- At 70 percent efficiency: 7.05 ÷ 0.70 × 0.03 = 0.302 dollars
- At 58.75 percent: 7.05 ÷ 0.5875 × 0.03 = 0.360 dollars
The same garment costs about 6 cents more to make at the lower efficiency. See our guides on how to calculate product cost and factory overheads for the full chain.
Why accuracy matters: a 5 percent error
Suppose the true SAM is 7.05 but a rushed study says 7.40, which is about 5 percent higher.
- The target at 70 percent would become 8,400 ÷ 7.40 = 1,135 pieces instead of 1,191, a drop of 56 pieces a day
- An operator who makes 1,191 pieces would show an efficiency of 1,191 × 7.40 ÷ 12,000 = 73.4 percent, instead of the true 70
- The quoted cost would be too high by 5 percent on the labour portion, which can lose an order
A SAM that is too low does the opposite. It sets targets that nobody can meet, and it hides a loss in prices. Our article on target versus actual production shows how that gap appears on the floor.
Other ways to get SAM
Stopwatch time study is the most direct method, but it is not the only one.
| Method | How it works | Notes |
|---|---|---|
| Stopwatch time study | Observe and time real operators | Needs trained observers and rating skill |
| Video time study | Record and time the video | Allows review and training |
| Predetermined time systems (PTS) | Break the task into basic motions with known standard times, using systems such as MTM or garment-specific data like GSD | Faster for new styles, needs trained users and licensed data |
| Work sampling | Random observations of activity | Good for allowances and delays, not for operation times |
| Historical data and style libraries | Reuse SAMs from similar past styles | Quick, but check differences in fabric and details |
| Software tools | Library-based SAM calculators | Depend on the quality of the library |
Many factories use predetermined times for a first estimate in the sampling stage and then confirm with a time study on the line.
Factors that change SAM
- Fabric type, weight and stretch
- Seam length and stitch density
- Machine type, speed and attachments
- Style details such as pockets, plackets, topstitching and trims
- Operator skill and training
- Bundle size, layout and workplace design
- Needle and thread quality
- Buyer quality standards and tolerances
When any of these change, the SAM may need a recheck. A new fabric or a new attachment is a good reason for a new study.
Common mistakes
- Timing one or two cycles and calling it a standard
- Timing the fastest operator and using a rating of 100 anyway
- Mixing the add-on and share-of-standard methods
- Leaving out the allowances
- Forgetting to separate machine time from handling time
- Copying a SAM from a different fabric or style
- Not updating the SAM after a method change
- Using a SAM for sewing only when the buyer expects a total including finishing
- Rating without a reference or training
A simple checklist
- List and describe every operation.
- Fix the method, machine and workplace.
- Choose a trained, typical operator.
- Time at least 10 cycles for each operation.
- Remove unusual cycles and average the rest.
- Apply a rating for pace.
- Add allowances using one agreed rule.
- Convert to minutes and sum for the garment.
- Check against similar past styles and buyer data.
- Record the study and review it after the first production run.
Final thoughts
Learning how to calculate standard allowed minutes gives you control over targets, efficiency and cost. Fix the method, time enough cycles, rate honestly, apply one clear allowance rule and add the operations up. Then check the figure against the first production run and correct it. A SAM that people trust makes the whole factory easier to plan.
Frequently asked questions
SAM = average observed time × rating ÷ 100 × (1 + allowance), converted to minutes.
They are often used for the same thing. Some factories use SMV for basic time without allowances and SAM for the time with allowances. Check the definition in your own factory.
At least 10 for short operations. More cycles give a steadier result.
Many factories use a total of 10 to 20 percent for personal needs, fatigue and delay. The right figure depends on the work, the factory and the buyer.
Target = operators × working minutes × efficiency ÷ SAM.
Efficiency = pieces made × SAM ÷ (operators × working minutes) × 100.
Usually the sewing SAM and the finishing SAM are counted separately, and cutting is separate too. State clearly what your SAM covers.